CE Certified Carton Flow Rack Factories & Exporter

Next-Generation FIFO Dynamic Storage Systems engineered for high-density warehouse picking, automated logistics integration, and structural safety compliance.

Engineered Carton Flow Solutions Showcase

Explore our CE-certified dynamic racking series engineered for seamless First-In, First-Out (FIFO) material movement.
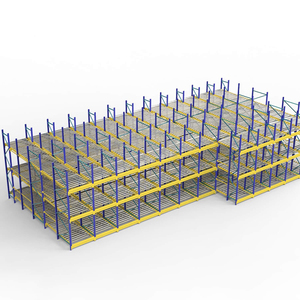
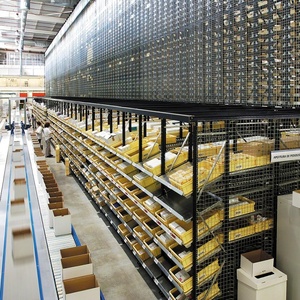
Customizable Heavy Duty Gravity Flow Racking System

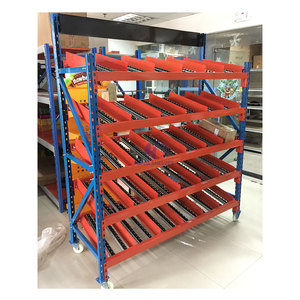
Mracking Heavy Duty Metal Gravity Flow Racks for Sale Customizable Gravity Flow Racking System

View Product Details
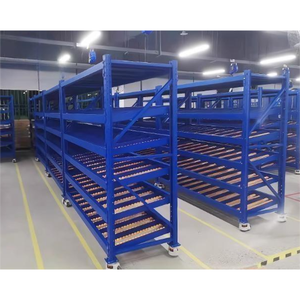
Heavy Duty Adjustable Carton Gravity Flow Rack

High Efficiency Durable Heavy Duty Adjustable 5-Layer Carton Gravity Flow Rack CE Certified Smooth For Distribution Centers

View Product Details
Customized Warehouse Gravity Carton Flow Rack

Customized Warehouse Storage Rack Pallet Flow Rack Shelving Lineside Roller Flow Rack Gravity Carton Flow Racking

View Product Details
Steel Warehouse Flow Rack System

High Density Heavy Duty Steel Durable Corrosion Protection Flow Rack System For Warehouse Storage

View Product Details
Carton Flow Rack Sliding Roller Shelf

Langle Carton Flow Rack System Sliding Roller Shelf for Warehouse Storage Slide Warehouse Rack

View Product Details
Gravity Carton Flow Rack FIFO

Gravity Flow Carton Flow Rack for Warehouse FIFO Storage System

View Product Details
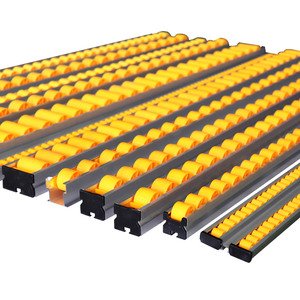
Gravity Flow Rail Roller Track

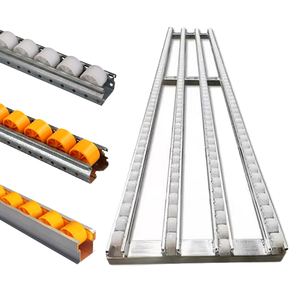
Gravity Flow Rail Roller Track PE ABS Wheel 200KG Load Carton Flow Rack FIFO Storage Sliding Shelf for Warehouse

View Product Details
Warehouse FIFO Gravity Carton Flow Rack System

Factory Warehouse Storage 5 Durable Gravity Flow Racking FIFO Adjustable Roller Rack Metallic Shelves Carton Flow Rack System

View Product Details
+300%
Picking Efficiency
60%
Floor Space Saved
100%
CE & EN Compliance
0 kWh
Gravity Powered Energy

Industrial Whitepaper: Structural Mechanics & CE Certification Standards

In modern high-throughput fulfillment hubs, cold chain centers, and fast-moving consumer goods (FMCG) distribution facilities, operational velocity hinges on intra-logistics efficiency. As global supply chains shift toward automated order picking and micro-fulfillment models, the traditional static shelving unit has become a structural bottleneck. Modern industrial engineering demands dynamic, self-replenishing material handling solutions. CE Certified Carton Flow Rack Systems stand at the critical intersection of physics-driven gravity movement, ergonomic layout design, and zero-carbon energy efficiency.

1. The Architectural Engineering of Dynamic Gravity Flow

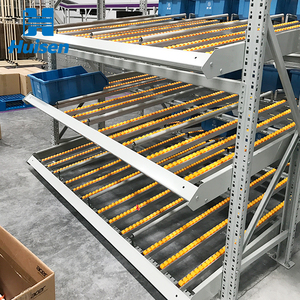
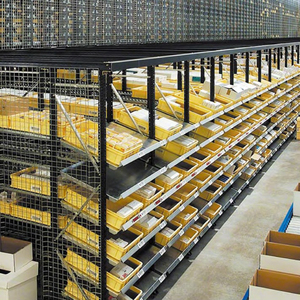
A carton flow rack—frequently termed a gravity flow racking system or roller track rack—operates on an inclined bed featuring engineered wheel tracks. Cartons, totes, and plastic containers are loaded from the rear loading aisle (replenishment face) and glide smoothly under controlled gravity down to the front picking aisle (discharge face). This structural segregation of stocking personnel and picking operators eliminates aisle congestion, enforces strict First-In, First-Out (FIFO) inventory rotation, and minimizes travel distance for warehouse personnel by up to 75%.

Core Mechanical Components & Metallurgical Integrity

  • Structural Cold-Rolled Steel Frames: Fabricated using premium Q235B or Q355B structural steel grades, our upright frames undergo precision roll-forming to withstand heavy static loading and dynamic impact from high-density stocking cycles.
  • High-Impact Polypropylene & ABS Roller Tracks: Engineered with low-friction coefficients, precision ball bearings, and high-impact structural polymers, individual track channels can support loads ranging from 50 kg/m up to 300 kg/m depending on roller density.
  • Adjustable Incline Channels & Beams: Featuring drop-in beam connectors with safety locks, our flow beds allow micro-pitch adjustments (typically at 50mm or 75mm increments). Incline gradients are calibrated between 2.5° and 5° depending on carton bottom friction coefficient, weight, and operational ambient temperatures.
  • Modular Lane Separators & Guide Rails: Zinc-plated or powder-coated steel lanes maintain trajectory alignment, preventing carton binding or off-center jams across multi-SKU shelf levels.

2. European Quality Benchmark: Decoding CE Certification & EN Standards

When procuring industrial racking systems at enterprise scale, safety accreditation is not merely a compliance checkbox—it is a mandatory risk mitigation parameter. Our OEM/ODM manufacturing operations strictly adhere to European Commission Directives, ensuring full CE Mark certification alongside strict compliance with structural engineering standards:

Standard Designation Engineering Domain Operational Impact & Compliance Benchmark
EN 15512:2020 Steel Static Storage Systems Rigorously defines structural design principles, load factor safety tolerances, and yield stress calculations under maximum bay loading.
EN 15635 Application & Maintenance of Storage Equipment Establishes safe operational thresholds, structural deflection limits (L/200), and systematic risk assessment protocols for damaged components.
ISO 9001:2015 Quality Management Systems Guarantees raw material traceability, robotic welding seam consistency, and automated powder coating thickness controls (>60 to 80 microns).
ISO 14001:2015 Environmental Management Ensures non-toxic, heavy-metal-free polyester powder coatings and sustainable energy recovery across our manufacturing plants.

CE Certification ensures that every structural upright, beam connector, and plastic wheel track has undergone finite element analysis (FEA) and dynamic stress testing. For international buyers, this guarantees structural stability under heavy operational loads, high seismic risk tolerances, and complete workplace safety protection against catastrophic rack collapses.

Procurement Insights & Industry Future Trends (2025–2030)

Strategic foresight for logistics planners, plant managers, and global supply chain directors.

Hybrid AMR & AGV Integration

Future procurement trends emphasize combining gravity carton flow racks with Autonomous Mobile Robots (AMRs). Gravity beds act as zero-energy buffer stations for robotic pickers.

Pick-to-Light & IoT Sensing

Modern enterprise flow racks are pre-engineered with integrated wiring channels for digital Pick-to-Light sensors, achieving 99.99% picking accuracy in high-velocity e-commerce hubs.

Eco-Polymer Roller Tech

Next-generation roller tracks feature recycled high-density polymers with ultra-quiet ceramic bearing inserts, reducing warehouse acoustic noise below 55 decibels.

Sourcing Matrix: Total Cost of Ownership (TCO) vs. Initial CapEx

Procurement directors traditionally evaluate warehouse storage on a simple "Cost Per Storage Position" basis. However, leading global supply chain strategists now utilize a Total Cost of Ownership (TCO) evaluation framework. While static shelving presents a lower initial CapEx, carton flow systems yield a payback period typically between 9 to 14 months based on the following operational yield improvements:

  • Elimination of Wasted Floor Space: By collapsing multiple access aisles into a single replenishment face and picking face, storage density increases by 60% to 150% within the same footprint.
  • Labor Cost Reduction: Order pickers spend less time walking and searching. Cartons present automatically at the pick face in an ergonomic position, reducing repetitive strain injuries (RSI) and workers' compensation liabilities.
  • Zero Electricity Operational Overhead: Unlike powered conveyor networks, gravity carton flow systems consume zero kilowatt-hours of power, providing direct alignment with corporate ESG (Environmental, Social, and Governance) targets.

Why Partner With Our Manufacturing Facilities

Direct Factory OEM/ODM Supplier backed by robust quality control, registered corporate transparency, and regional project execution capabilities.

As a certified manufacturing power (Operating under registered entity SSM 202201004215 / 1449912-V), our manufacturing ecosystem seamlessly integrates structural engineering design, continuous steel roll-forming, robotic welding, and automated surface treatment. We serve global clients across Southeast Asia (including dedicated installation hubs in Malaysia and Singapore), Europe, North America, and the Middle East.

Core Manufacturing Competencies

  • End-to-End Production Control: We do not outsource critical cold-rolling or stamping processes. From raw coil slit testing to final packaging, every component is manufactured in-house under strict ISO 9001 supervision.
  • Custom Structural Engineering (CAD/BIM): Our structural engineering team delivers 3D layout consultation, floor loading structural calculations, and Building Information Modeling (BIM) files to seamlessly integrate with your general contractor's building design.
  • 18000 Series Interservice & Lifecyle Maintenance: Beyond manufacturing, we provide complete post-installation support, periodic rack inspections, damage assessment reports, and certified replacement components to keep your site fully compliant.
  • Global Logistics & Export Readiness: Products are packaged using export-grade steel bundling, corner protection, and moisture-barrier shrink wraps to guarantee zero transit damage across international ocean routes.

Frequently Asked Questions (Procurement & Engineering FAQ)

Expert technical answers addressing common structural, operational, and procurement queries.

Q1: What structural variables determine the pitch angle (incline) of a carton flow rack?
The optimal flow bed pitch typically ranges from 3% to 5% (approximately 1.7° to 2.9°). The precise angle depends on carton weight, bottom material rigidity (corrugated cardboard, molded polypropylene, or wood), roller track bearing resistance, and ambient storage temperatures (e.g., cold storage environments require slightly steeper inclines to offset lubricant viscosity). Our engineering team conducts physical flow testing with sample customer cartons prior to final factory manufacturing.
Q2: How does a carton flow rack differ structurally from a heavy-duty pallet flow rack?
While both rely on gravity movement, carton flow racks are engineered for hand-loaded cartons, totes, and small parts bins (typical loads: 50kg to 300kg per shelf level). They utilize lightweight high-impact plastic or aluminum roller tracks mounted on adjustable intermediate beams. Pallet flow racks utilize heavy steel full-width rollers or dual-track steel wheels designed for forklift-loaded wooden/plastic pallets weighing 500kg to 1500kg per pallet position, incorporating speed controllers and mechanical brake rollers.
Q3: Are your carton flow racking systems certified for international export and building safety codes?
Yes. All structural steel members, upright frames, shelf beams, and dynamic roller track assemblies carry full CE Mark accreditation. Our design and structural calculation methods follow European EN 15512 standards and American RMI (Racking Manufacturers Institute) guidelines, ensuring compliance with international building codes, fire safety clearance requirements, and workplace health and safety (OSHA) standards.
Q4: Can carton flow tracks be integrated into existing selective pallet racking systems?
Absolutely. Our carton flow bed modules are designed for universal retrofitting. Utilizing universal mounting brackets, our roller tracks and bed frames can be installed into your existing standard selective pallet rack step beams or box beams. This retrofitting transforms lower racking levels into high-density carton pick modules while preserving upper rack levels for bulk pallet storage.
Q5: What is the typical production lead time for enterprise OEM orders, and do you offer installation?
Standard manufacturing lead time for full container loads (FCL) ranges between 15 to 25 business days depending on customized powder coating specifications and lane configuration complexity. We provide comprehensive installation support: for domestic regional projects (such as Malaysia and Singapore), our certified in-house crews manage complete site assembly and leveling. For global export destinations, we provide detailed 3D installation blueprints, step-by-step video tutorials, and optional remote or on-site supervisory engineering support.
Q6: What maintenance protocols are required to ensure long-term operational safety?
Carton flow systems require minimal mechanical maintenance due to their gravity-powered design. However, best practice safety protocols include monthly visual inspections of roller tracks for debris, verification of beam safety lock retention clips, checking end-stop brake integrity, and checking for beam deflection under uniform load. Through our 18000 Series Interservice program, we provide formal structural inspection checklists and rapid replacement component delivery worldwide.
Q7: How do you prevent carton impact damage at the picking face?
To prevent carton crushing or momentum surge at the discharge face, our flow tracks can be equipped with engineered mechanical impact dampers, decelerator rollers, or gradual tilt trays. Tilt trays present cartons at an ergonomic angle (typically 15° to 30°) for rapid visibility and single-item picking while absorbing kinetic impact energy from incoming rear cartons.

Accelerate Your Warehouse Logistics Performance

Ready to optimize your warehouse picking velocity, reduce labor overhead, and implement CE-certified dynamic storage? Connect with our senior structural engineering team today for a free CAD layout design and direct OEM quotation.

Contact Us
+60 11-3302 1235[email protected]