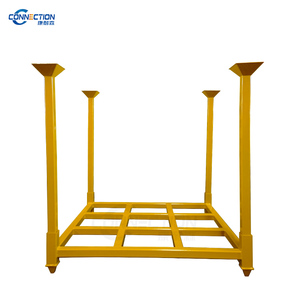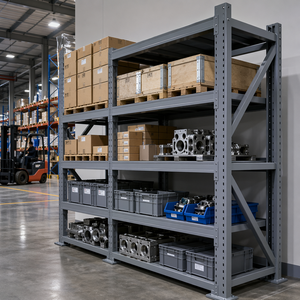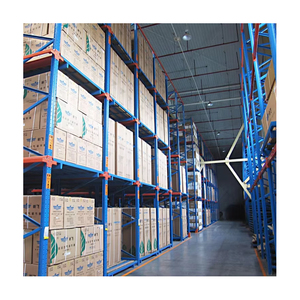
Direct from Certified OEM Manufacturers: Heavy-Duty Structural Cantilever Racks, Euro Pallets, Column Impact Barriers, and Modular Storage Frameworks.
Managing long, heavy, or irregular materials such as steel pipes, PVC tubing, aluminum extrusions, and industrial conduit requires specialized storage architecture. Standard pallet racking systems lack the lateral support and clear span needed to prevent material sagging, bending, or structural damage. As leading CE Certified Pipe Racking System Manufacturers & Factory engineers, our enterprise develops specialized heavy-duty Cantilever and Roll-Out Pipe Racks designed specifically for maximum vertical space optimization and seamless material handling access.
Our manufacturing protocols adhere strictly to international quality frameworks, including ISO 9001:2015 for quality management and ISO 14001 for environmental stewardship. Every structural column, cantilever arm, and base connector undergoes rigorous Finite Element Analysis (FEA) to ensure mechanical safety under extreme static and dynamic loading. Whether your operational facility requires light-duty manual racking or fully automated high-density shuttle integration, our factory delivers customized OEM/ODM structural steel configurations tailored to your exact warehouse footprint.
Our integrated manufacturing facility located in Shah Alam operates as an end-to-end engineering center. We manage every phase of rack production internally—from raw steel coil slitting and automated robotic welding to electrostatic powder coating and final compliance inspection. Partnering directly with a verified direct manufacturer ensures full supply chain transparency and eliminates intermediary markups.
Selecting the correct pipe racking configuration depends on pipe outer diameter (OD), wall thickness, bundle weight, stack height, and material handling equipment (e.g., side-loaders, overhead cranes, or standard forklifts). Below is our standardized factory specification matrix for heavy-duty structural pipe cantilever systems:
| Structural Parameter | Light-to-Medium Duty Series | Heavy-Duty Cantilever Series | Automated / Roll-Out Pipe Racks |
|---|---|---|---|
| Target Application | Plastic PVC Pipes, Copper Tubing, Light Extrusions | Structural Steel Pipes, Oil & Gas Casing, Bundled Tubes | High-Density Crane-Operated Pipe Storage |
| Material Grade | Cold-Rolled Steel Q235B | Hot-Rolled Structural Steel Q355B / H-Beams | High-Yield Structural Alloy Steel |
| Load Capacity per Arm | 200 kg – 800 kg | 1,000 kg – 5,000+ kg | 2,000 kg – 10,000 kg (Drawer system) |
| Column Height (Max) | Up to 4.5 Meters | Up to 12.0 Meters | Custom Height per Overhead Crane clearance |
| Surface Finishing | Dry Powder Coating (RAL Standard) | Hot-Dip Galvanized (Outdoor / Anti-Rust) | Thermally Cured Epoxy Polymer Coating |
| Safety Certifications | ISO 9001:2015, CE Marking | CE, EN 1090-2, OSHA Structural Standard | CE, ISO 9001, FEM 10.2.09 Compliant |
The global industrial storage ecosystem is undergoing a major transformation driven by supply chain resilience, space optimization imperatives, and automated material handling integration. Procurement managers sourcing pipe racking systems are increasingly focusing on modern engineering requirements:
1. Integration with Automated Roll-Out & Crank-Operated Systems: Traditional static cantilever racks require wide aisles for forklift maneuvers. Modern facility designs prioritize roll-out cantilever racks where arms extend 100% horizontally via mechanical cranks or electric motors. This allows overhead cranes to load and unload long pipes vertically, reducing required floor space by up to 50%.
2. Structural Safety and Impact Prevention Systems: Warehouse safety regulations (such as OSHA and European EN standards) have become significantly stricter regarding structural rack collisions. The integration of polymer safety barriers, such as flexible HDPE column protectors and heavy-duty steel guardrails, is now standard practice in high-traffic logistics environments to prevent catastrophic forklift impacts.
3. Sustainable & Recycled Storage Accessories: Environmental ESG targets are pushing logistics hubs to incorporate sustainable materials. Upgrades include using recycled high-density polyethylene (HDPE) euro pallets for component transport, non-toxic powder coating processes, and scrap-reducing modular steel framing designs.
Direct answers from our structural engineering team on pipe racking procurement, safety compliance, and OEM customization options.
CE Certification verifies that the structural racking system meets strict European health, safety, and environmental protection standards (such as EN 1090-2). It guarantees that structural calculations, steel yield strength, and weld quality have undergone independent testing and verification, protecting your facility against structural failures and legal compliance risks.
Roll-formed steel is made from thin-gauge sheet steel shaped at room temperature, ideal for light-to-medium hand-loaded shelving. Structural steel racks are constructed from hot-rolled solid steel I-beams or H-beams, providing far superior resistance to heavy impact, twisting, and heavy concentrated pipe bundle loads.
Yes. As a direct OEM manufacturer, we design and produce custom column heights, arm lengths, pitch spacings, and load capacities based on your specific material length (e.g., 6m, 12m standard pipe bundles) and facility ceiling height.
Our cantilever arms can be equipped with removable structural steel pipe stops (stoppers) at the arm tips. Additionally, incline arms (sloped backward at 2° to 5°) can be integrated to ensure round pipes remain stable during loading and retrieval.
To prepare an accurate proposal, our engineering team needs: 1) Overall dimensions and weights of your pipe bundles; 2) Available building floor plan & clear height; 3) Type of forklift or crane used; and 4) Indoor or outdoor installation site environmental conditions.