Explore our certified racking assemblies, stackable post pallets, spool management systems, and pre-engineered industrial mezzanines engineered for severe operational payloads.
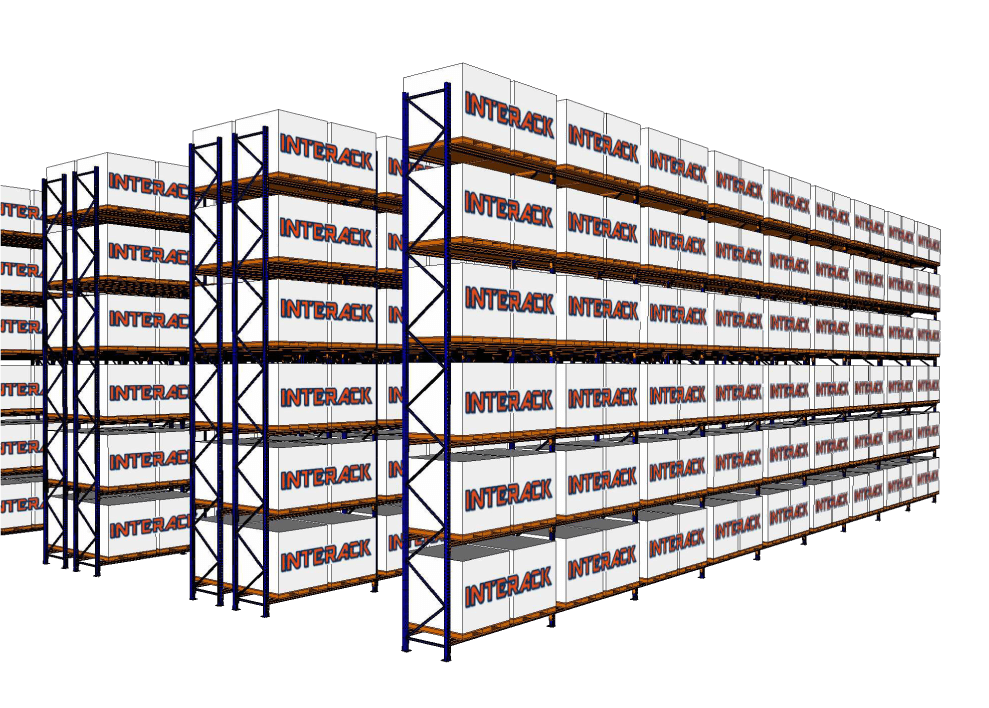
In conventional warehouse spatial topologies, static selective pallet racking dedicates between 55% and 65% of the total cubic footprint entirely to operating access aisles. This geometric inefficiency drives up real estate capital expenditure, inflates HVAC overhead in climate-controlled environments, and imposes strict ceilings on SKU density. Heavy-Duty Mobile Racking Systems (MRS) overcome this limitation by mounting heavy superstructure pallet rack bays onto motorized chassis bases that glide smoothly over high-tensile embedded floor guide rails.
Through state-of-the-art multi-wheel synchronous drive assemblies, Variable Frequency Drives (VFD), and programmable logic controllers (PLC), an entire block of 10 to 30 racking runs requires only one dynamic operational aisle. When an operator or an automated Reach Truck / Automated Guided Vehicle (AGV) commands access via RF remote control, optical sensory inputs, or Warehouse Management System (WMS) APIs, the motorized carriages traverse laterally in unison, creating an aisle exactly where required in under 35 seconds.
This volumetric density shift delivers up to an 85% surge in pallet position capacity within the identical building footprint, or conversely, reduces the required building volume by 45% for greenfield developments. For pharmaceutical cold stores, deep-freeze logistics (-30°C), and bonded port facilities, this compaction drastically slashes thermodynamic thermal transfer, minimizing industrial refrigeration power consumption by up to 40%.
A rigorous engineering comparison between static pallet racking, drive-in systems, motorized mobile racking, and automated mini-load AS/RS systems.
| System Architecture | Volumetric Efficiency | SKU Selectivity | Forklift Compatibility | Cold Store Energy Savings | Civil Floor Slab Requirement | Relative CAPEX / Pallet |
|---|---|---|---|---|---|---|
| Standard Selective Static Racking | 40% – 45% | 100% (Instant) | Standard Counterbalance / Reach | Low (Baseline Zero) | Standard Industrial Slab (Class 2) | Low (1.0x Base) |
| Drive-In / Drive-Thru Racking | 65% – 70% | Low (LIFO / Strict FIFO) | Specialized Narrow Counterbalance | Moderate (+15% Compaction) | Standard Reinforced Slab | Low-Mid (1.3x Base) |
| Motorized Mobile Pallet Racking (MRS) | 80% – 88% | 100% (Aisle Driven) | Standard Reach / VNA Trucks | Exceptional (35% - 42%) | Precision Recessed Rails (DIN 18202) | Moderate (2.2x Base, Fast ROI) |
| Radio Shuttle High-Density System | 75% – 82% | Medium (Batch FIFO/LIFO) | Standard Forklifts + Auto Cart | High (+28% Compaction) | Standard Level Slab | Mid-High (2.5x Base) |
| Full Automated High-Bay AS/RS | 88% – 95% | 100% (Automated) | Fully Automated Stacker Cranes | High (+35% Compaction) | Deep Foundation & Sub-Millimeter Slab | High (5.0x – 8.0x Base) |
*Calculations based on standard 1,200mm × 1,000mm ISO/Euro pallets with 1,000 kg nominal payloads. Volumetric efficiency accounts for non-storage flue space, vertical clearances, and transfer bays.
Key technological, regulatory, and environmental paradigms shaping procurement specifications for intralogistics infrastructure over the next decade.
Global net-zero regulations are forcing refrigerated storage operators to cut energy footprints. Mobile racking has become the default structural standard for cold logistics hubs, shrinking conditioned cubic volumes and slashing peak electrical cooling demand by upwards of 40%.
Procurement teams are moving away from isolated mechanical racks toward integrated sensor-ready platforms. Modern mobile carriages now feature digital PLC gateways that coordinate directly with Autonomous Mobile Robots (AMRs), automatically clearing aisles ahead of robotic picking cycles.
International procurement frameworks now evaluate structural suppliers on environmental transparency. Top-tier Chinese exporters are transitioning to high-yield Q355B cold-rolled steel with Environmental Product Declarations (EPD) and solvent-free electro-static powder coatings.
Clients in seismically active regions (Pacific Rim, Middle East, Mediterranean) demand rigorous finite element dynamic analysis. Exporters must prove load-bearing resistance under dynamic ground acceleration under ASCE 7-22, Eurocode 8, and NZS 4219 standards.
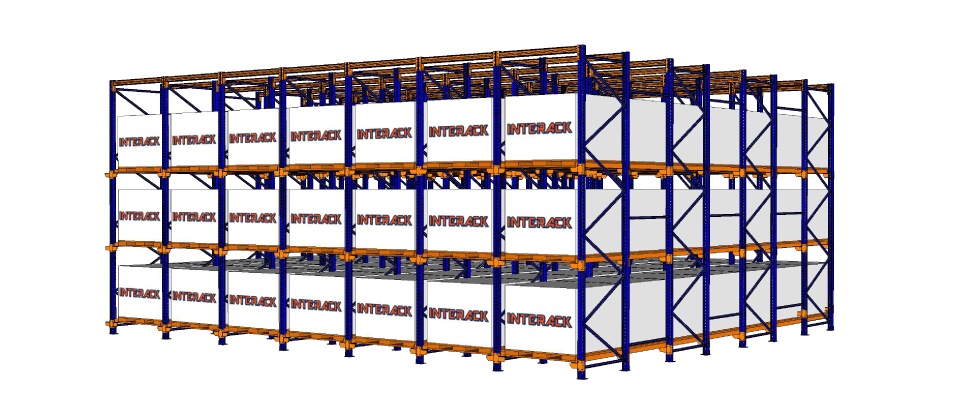
When deploying motorized systems carrying up to 1,000 metric tons of steel and inventory across a continuous mobile block, occupational safety is paramount. Our export-grade mobile racking systems integrate an exhaustive multi-level safety circuit designed to meet the rigorous European Machinery Directive 2006/42/EC and EN 15095 standards.
Every motorized carriage is outfitted with continuous optical safety light curtains at the open aisle entrance. If a forklift, warehouse operator, or foreign object breaks the optical infrared perimeter while the carriages are in transit, the PLC triggers an instantaneous electromagnetic brake deceleration within 0.25 seconds.
Mechanical fail-safes complement the electronic mesh: full-length foot-level trip bars running along the chassis perimeter immediately cut circuit power upon physical contact. Low-temperature rated industrial geared motors with variable frequency ramp-up prevent pallet tipping during starts and stops, while acoustic horns and flashing strobe beacons warn personnel before any motorized movement begins.
Custom structural configurations tailored to payload weight, inventory turnover speed, packaging formats, and ambient environmental conditions.

High-capacity upright frames designed for raw materials, heavy tooling dies, and work-in-progress components. Engineered to handle point loads exceeding 4,000 kg per beam level with integrated collision protection.

Ultra-dense layouts specifically engineered for multi-temperature cold storage (-30°C to +4°C). Provides 100% pallet selectivity while reducing conditioned airspace to cut facility utility costs dramatically.

Rapid carton replenishment and multi-tier picking structures. Integrates seamlessly with pick-to-light systems and overhead mezzanine floors to maximize omnichannel order assembly speed.
High-turnover FMCG logistics racks designed for rapid forklift staging, pallet flow compatibility, and zero-downtime structural integrity under continuous round-the-clock shift cycles.

High-density mobile shelving compactors for banking records, legal files, pharmaceutical samples, and museum artifacts. Clean, dust-sealed construction with electronic pin-code access security.

Flexible boltless rivet and longspan shelving designed for light industrial workshops, automotive dealerships, and maintenance rooms requiring reconfigurable shelving heights without special tools.
Combining heavy automated manufacturing capacity, strict global quality standards, and full lifecycle engineering support for seamless project handovers.
Equipped with high-precision CNC cold-roll-forming lines, automated laser tube cutters, robotic multi-axis welding cells, and continuous shot-blasting powder-coating systems for superior dimensional accuracy and finish quality.
Full manufacturing alignment with ISO 9001:2015 quality assurance and ISO 14001 environmental standards. Every heat of steel undergoes certified tensile yield tests and Charpy V-notch impact testing for sub-zero applications.
Our senior structural engineering team develops customized 3D BIM models, slab load deflection analyses, and forklift aisle sweep simulations to optimize every square meter before manufacturing commences.
Comprehensive lifecycle maintenance, periodic safety audits, acoustic laser rail re-alignment, and rapid replacement component dispatch to keep your mission-critical installations fully compliant with safety codes.
Specialized maritime export steel racking packaging protocols. Uprights and beams are bundled with protective edge sleeves and precision container pack-plans that maximize container volume and prevent transit abrasion.
Trusted by multinational logistics giants, electronics manufacturers, and major automotive OEMs across Southeast Asia, the Middle East, Europe, and the Americas for large-scale high-bay racking systems.
Expert engineering answers to critical inquiries regarding floor slab capacity, cold store integration, safety certifications, and installation logistics.
Heavy mobile racking systems require floor slabs with high point-load capacity and strict flatness tolerances conforming to DIN 18202 Group 4 standards. Recessed floor guide rails are either embedded in structural trenches during the primary slab pour or diamond-cut into existing cured slabs, leveled with precision leveling bolts, and backfilled with non-shrink high-strength epoxy grout (compressive strength ≥ 70 MPa).
For sub-zero cold rooms, our mobile carriages feature low-temperature synthetic lubricants, silicone wiring jackets resistant to thermal embrittlement, IP65-sealed PLC electrical cabinets with internal dehumidifying heaters, and cold-impact tested Q355D structural steel. This guarantees zero condensation short-circuits and prevents brittle steel failure during continuous freezing operations.
Multiple independent safety systems run in parallel: (1) Active photoelectric light grids that scan the entry face of every open aisle; (2) Full-length mechanical trip bars at floor level on each mobile base; (3) Ultrasonic proximity sensors on carriage ends; and (4) Accessible emergency push-button stations on all front control panels. Interruption of any sensor immediately halts carriage motion within milliseconds.
Each chassis carriage uses electronic wheel synchronization controlled by decentralized variable frequency inverters and optical rotary encoders. The drive shafts link heavy-duty forged steel wheels on guide rails (machined convex profile) and flat idle wheels (cylindrical profile), eliminating mechanical crabbing and skewing even under asymmetric bay loading.
Yes. If your existing upright frames and load beams comply with current structural steel codes and match our mobile chassis bolt-hole patterns, we can manufacture the motorized mobile undercarriages, floor rails, and control panels to mount your existing rack superstructures, significantly lowering conversion capital expenditure.
Standard manufacturing lead times range from 4 to 7 weeks depending on total bay count and rail lengths. Our engineering team prepares optimized 3D container stuffing diagrams for 40ft High Cube (HC) shipping containers, typically achieving 24 to 26 metric tons per container while securing all precision-machined motorized carriages on specialized timber saddles.
Our heavy storage installations and custom racking systems are deployed worldwide across Fortune 500 manufacturing plants, regional 3PL hubs, and multinational retailers.